Description
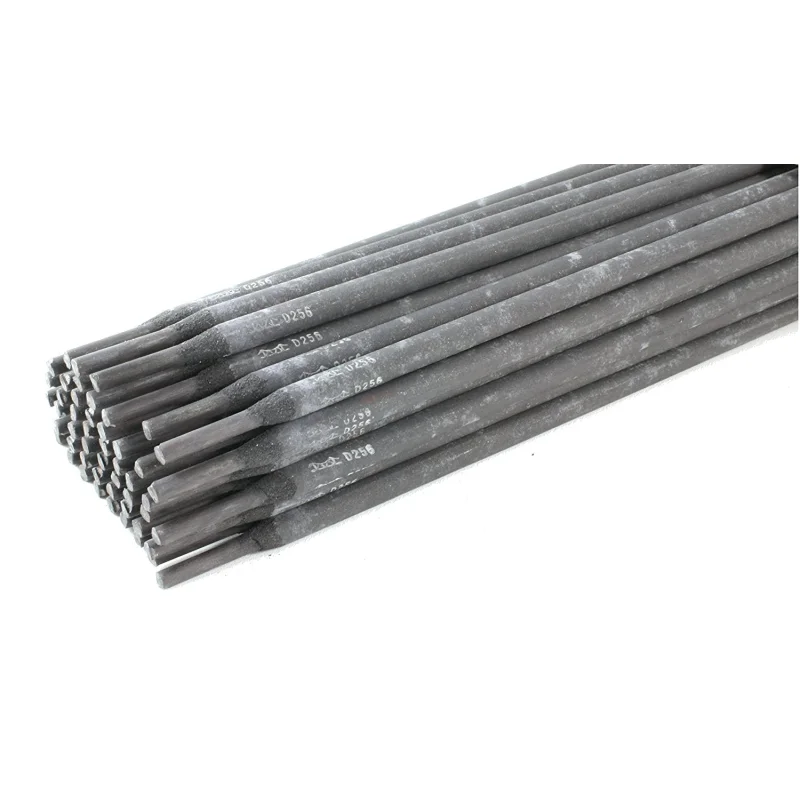
- Introduction: D256 is a high manganese steel surfacing electrode with low hydrogen potassium type coating AC/DC. (When AC welding, Open circuit (no load) voltages of arc welding should be higher than 70V).
- When surfacing use low current, narrow bead, hammer or water quench immediately when hot to reduce crack tendency. use in austenitic high manganese steel Recommendations for welding: Austenitic manganese steels, in as cast condition or as weld metal, are sensitive to hot shortness and may crack if subjected to excessive heat.
- Under normal conditions the base material should not be preheated and interpass temperatures above 200 C should be avoided. Welding outdoor in very cold weather, the base material should be warmed up to 50-100 C.
- Weld metal hardness, (all weld metal): As welded….180-200 HB. (no preheat, interpass temperature 100-150 C.) Work hardened…44-48 HRC.
- (About 25 % degree of reduction.) Machinability: Grinding is normally applied. Overheating must be avoided.
- Redrying the electrodes: 200 C, 2 h. D256 is a high manganese steel surfacing electrode with low hydrogen potassium type coating AC/DC+ Weld metal hardness, (all weld metal): HB 170 Min AC OCV: 70 – Polarity: AC, DC + Applicationused for surfacing welding on abrasion parts of all kinds of crushers, high-manganese steel rails, buckets, bulldozers, etc You will receive 11 Lb of 14″L x “””1/8” Electrodes